ISO 9001:2015 ACS-QMS Certified

Three Decades of Water Treatment Expertise

For more than 30 years, Radiant Chemical has been a reliable partner for industries that require advanced water treatment solutions.

On-Site Laboratory Diagnostics
Authorized Global Principals
Dedicated Field Support

Solving Water Challenges Since 1991

Explore Now

Our leadership in the market is built on satisfying today's needs and anticipating tomorrow's problems.

Water problems like scale, fouling, and corrosion damage industrial equipment. Radiant Chemical helps industries prevent these problems with proven treatment chemicals, reliable equipment, and on-site technical support for boilers, cooling towers, chillers, and generators, as well as reverse osmosis systems, ion exchange resins, and more. Since its establishment in 1991, the company has grown a substantial client base.

Protecting Critical Capital Equipment

Custom formulations and proven treatments engineered to prevent scale, combat fouling, and eliminate corrosion across industrial boilers, chillers, and cooling loops.
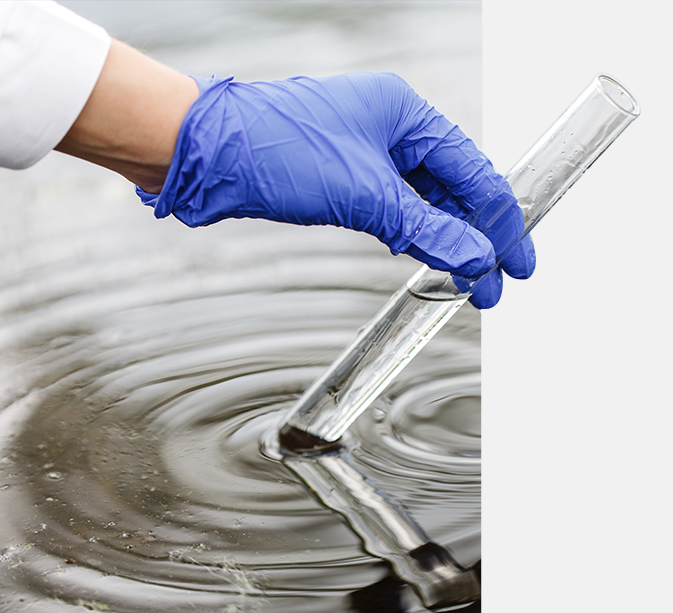
Radiant Chemical Industrial Water Specialists

33+ Years Proven Legacy

Since its establishment in 1991, Radiant Chemical has grown a substantial client base across Pakistan's leading industrial enterprises.

100% On-Site Support

Reliable equipment, routine water diagnostics, membrane testing, and full technical support from senior chemical engineers.
Explore Our Reliable Water Treatment Solutions

Our capabilities cover boilers, cooling towers, chillers, reverse osmosis, ion exchange, ultrafiltration, generators, and more.

Water Treatment Chemicals

Specialized water treatment products to protect your equipment from damage.

Water Treatment Plants & Equipment

Reliable systems engineered for consistent water quality and performance.

Wastewater Recycling & Reuse

Turn industrial wastewater into a sustainable resource with Radiant’s expertise.

Meet Our Global Technology Partners

We collaborate with the world’s eminent technology innovators to bring top-notch water treatment systems to Pakistan.

DuPont Water Solutions

DuPont Water Solutions

Global leader in FilmTec™ Reverse Osmosis, Nanofiltration, and Ion Exchange Resins.

Bio-Microbics USA

Bio-Microbics (USA)

Pioneers in advanced FAST® decentralized wastewater and biological treatment systems.

Jacobi Carbons Sweden

Jacobi Carbons (Sweden)

The world's largest manufacturer of coconut-shell and mineral activated carbons.

Polymem France

Polymem (France)

Foremost European specialist in hollow fiber Ultrafiltration (UF) membranes.

FPturbo Germany

FPturbo (Germany)

High-performance gas turbine compressor wash solutions and efficiency restoration.

Proud to Be Trusted by Leading Names

Multiple top-tier industrial conglomerates and multinational corporations rely on Radiant Chemicals for their specific water requirements.

Shan Foods
Pakistan Beverage Limited (PBL)
Pakistan Petroleum Limited (PPL)
Gul Ahmed Textile Mills
Lucky Energy
Candyland - Ismail Industries
Bisconni
Hilal Foods
Lakhany Silk Mills (LSM)
Nimir Chemicals Pakistan Ltd.
Saima Packaging
Zaman Textile Mills

Discover The Radiant Advantage

Every solution is built around your operational needs, with a focus on making better use of water, energy and equipment.

33 + Years of Proven Expertise

With over 33 years in the industry, we have the experience to solve your toughest water challenges.

Commitment to Quality

The company’s performance in the market is backed by its dedication to offering the best quality and service.

Reduced Operating Costs

We help you find ways to cut your operating costs and provide maximum return on your chemical investment.

Genuine Global Technology

Direct partnerships with globally renowned brands enable us to offer top-notch products and solutions.

Full Technical Support

You get full technical support from our experts in choosing, applying, and optimizing your treatment programs.

Custom Engineered Formulations

We combine our technical expertise and field experience to create custom solutions for your specific requirements.

Serving Multiple Industries Across Pakistan

Different sectors, different challenges, same expectation: water systems that don’t interrupt operations.

01
Process Water & Food Safety

Food & Beverage

Consistent process water, steam for cooking, pasteurization, and sterilization, and reliable refrigeration to protect product safety and reduce costly downtime.

02
High-Purity Specs & Compliance

Pharmaceutical

Water that consistently meets specifications, stable temperature control for chemical reactions and formulation, and steam quality that supports sterilization and clean-in-place systems for compliance.

03
Steam, Softening & Water Reuse

Textile

Reliable steam for dyeing, drying, and finishing, soft water for consistent quality, and color removal that enables water reuse and lowers discharge costs.

04
Steam Cycle & Turbine Cooling

Power & Utilities

Protected steam cycle efficiency for turbine generation, reliable cooling, and high-purity feedwater to reduce fuel consumption and the risk of unplanned outages.

05
Distillation & Continuous Cooling

Chemical

Steam for distillation and reaction heating, stable water quality, and efficient cooling to keep production continuous and operating costs controlled.

06
Rinse Quality & Compliant ETP

Metal

Consistent cooling and rinse water quality that reduces defects and rework, plus compliant wastewater treatment to lower environmental risk.

Case Studies: Measurable ROI in Action

Real operating data from manufacturing enterprises across Pakistan. See how custom chemical regimes, advanced membrane filtration, and on-site engineering teams eliminate downtime and conserve millions of gallons.

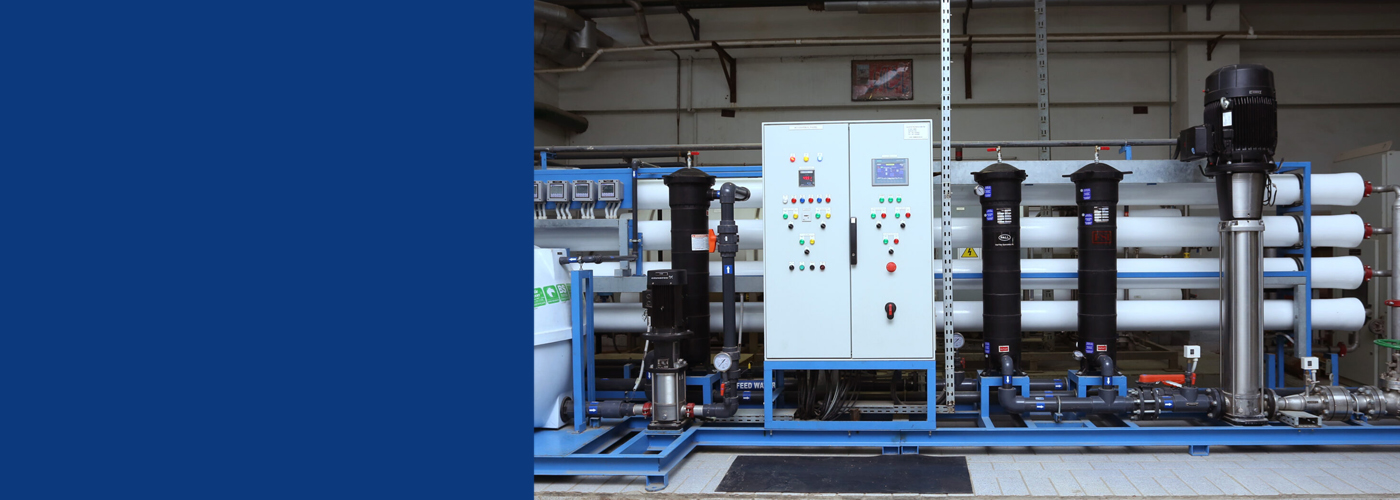
Industrial RO Water Recovery Train at Textile Mill
Textile & Dyeing Karachi Industrial Area

Eliminating Boiler Scaling & Reclaiming 65% Process Water

High TDS feed water and heavy hardness were causing severe boiler tube scaling, high fuel burn, and excessive blowdown losses. Radiant Chemical engineered custom anti-scalant chemistry alongside an automated RO recovery train, recycling 120,000 gallons daily with zero tube downtime.

65%
Water Recycled
Zero
Unplanned Outages
34%
Fuel Cost Saved
Cooling Water Biofilm Elimination at Bottling Facility
Food & Beverage National Bottler · Lahore

Complete Biofilm Removal & 4.5M Gallons Annual Water Savings

Persistent microbiological fouling across 4 cooling towers reduced chiller heat transfer efficiency and spiked power consumption. Radiant implemented a food-grade non-oxidizing biocide program with automated redox dosing, eradicating slime and reducing chemical consumption by 28%.

99.9%
Biofilm Removal
4.5M
Gallons Saved / Yr
28%
Chemical Reduction
High Pressure Steam Boiler Chemistry for Turbines
Power & Utilities Cogeneration Hub

Eliminating Turbine Silica Carryover in 45-Bar Steam Boilers

Volatile silica deposition on high-speed steam turbine blades forced costly shutdowns every 9 months. Radiant Chemical engineered an all-volatile boiler chemical treatment program and polisher resin regeneration protocol, maintaining steam silica below 0.01 ppm and extending maintenance intervals.

< 0.01
ppm Steam Silica
3+ Yrs
Between Overhauls
100%
Turbine Availability
Pharmaceutical Purified Water Validation Diagnostics
Pharmaceutical Sterile Facility · Islamabad

Purified Water (PW) Overhaul & Zero Microbial Contamination

A high-volume parenteral medicine manufacturer faced fluctuating conductivity and bioburden counts in their RO loop. Radiant Chemical deployed sanitary RO membrane retrofits, automated chemical sanitization protocols, and continuous monitoring, achieving uninterrupted cGMP audit pass rates.

< 1.1
µS/cm Conductivity
Zero
Batch Losses
100%
cGMP Audit Pass

Ready to Optimize Your Industrial Water Systems?

Schedule a comprehensive, complimentary on-site water audit with our senior chemical engineers. We test your feed water, inspect boilers, cooling loops, and RO membranes, and deliver an actionable efficiency plan with zero obligation.
Immediate Technical Hotline
Karachi Head Office: (92-21) 34540218, 34150518
Lahore Regional Office: (92-21) 34546245 (Ext. Lahore)
Engineering Inquiries: info@radiantchemical.com